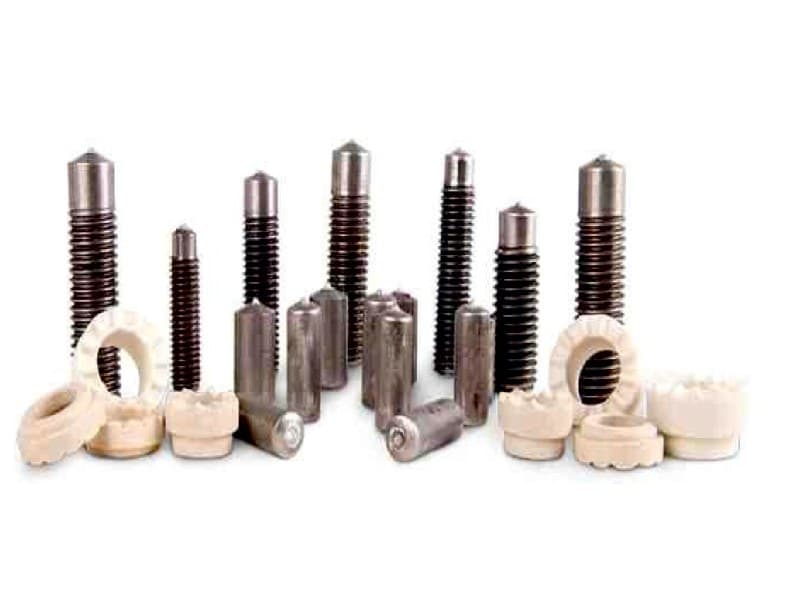
Stainless steel drawn arc studs
For earthing points, bonding and fittings that have to stay clean and corrosion-free on outdoor tanks and panels.
- Material
- Stainless steel
- Thread
- M8 · M10 · M12, others on request
- Supplied with
- Matched ceramic ferrule
■ Precision engineering & manufacturing · Hyderabad
Stainless and mild steel weld studs with matched ceramic ferrules, plus MS and PW bosses made to drawing. Built for transformer, switchgear and boiler manufacturers.

00About us
Hyderabad Engineering Works is a precision engineering and manufacturing company in Balanagar, Hyderabad. We make drawn arc weld studs, the ceramic ferrules they weld with, and custom bosses for manufacturers of transformers, switchgear, boilers and fuel-injection equipment.
Every part is made to your size, material and drawing, and our quality and safety systems are certified to ISO 9001:2015 and ISO 45001:2018.
01Product range
Studs are supplied with ferrules matched to them. Lengths, grades and non-standard sizes are made to order.
For earthing points, bonding and fittings that have to stay clean and corrosion-free on outdoor tanks and panels.
The workhorse for brackets, supports, clamps and internal assemblies on mild-steel tanks, enclosures and pressure parts.
Each stud is paired with a ferrule sized to it. The ferrule holds the arc, contains the molten pool and shapes a clean, even fillet.
Bosses made to your drawing, in the sizes your build calls for. Custom engineering for the fittings a standard catalogue does not cover.
02How it works
The stud is welded from one side, straight onto the plate. No hole, no nut on the back, and a fused joint across the full section of the stud.
Step A
The stud is loaded into the weld tool with its ceramic ferrule and set squarely against the base metal.
Step B
The trigger is pressed. The stud lifts off the plate and draws a controlled pilot arc, then the main arc.
Step C
When the arc period ends, the stud is driven into the molten pool the arc has formed on the plate.
Step D
The weld solidifies, the tool is withdrawn and the ferrule is knocked off, leaving a full-section fillet ready for inspection.
Section A–A · simplified
Why drawn arc
The whole cross-section of the stud fuses to the plate. The joint carries the full load the stud is rated for.
No hole goes through the wall, so oil-filled tanks and pressure parts stay sealed.
No crevice behind a nut or through-bolt for moisture to sit in.
A fused joint does not work loose from hum, noise or road transport the way bolted fittings can.
No drilling, no tapping, no backside nut. Weld onto a closed tank from the outside.
A weld takes under a second, and every stud is set to the same current and time.
03In a transformer
Permanent attachment points for earthing, mounting and internal assembly. Tap a marker to see what each stud carries.
Location 01
Studs on the tank wall take earth straps and grounding cables.
04Industries
We supply manufacturers across heavy electrical and process engineering, from single prototype batches to running production.
Earthing, accessory, bracket and internal-assembly studs for transformer tanks and covers.
Mounting and earthing studs for enclosures, busbar supports and panel hardware.
Studs and bosses for insulation, cladding and fittings on shells and ducts.
Precision-machined components made to the tolerances fuel systems demand.
Custom studs, bosses and engineered parts made to drawing.
05Why choose us
Components made to the dimensions and tolerances on your drawing, batch after batch.
Sizes, materials and bosses customised to the requirements of your industry.
A commitment to timely delivery and responsive customer service.
State-of-the-art equipment and current manufacturing techniques on the shop floor.
06Contact us
Tell us the stud, size and quantity, or send a drawing for bosses and custom parts. Our sales team will come back to you with a quote.
Enquiry form